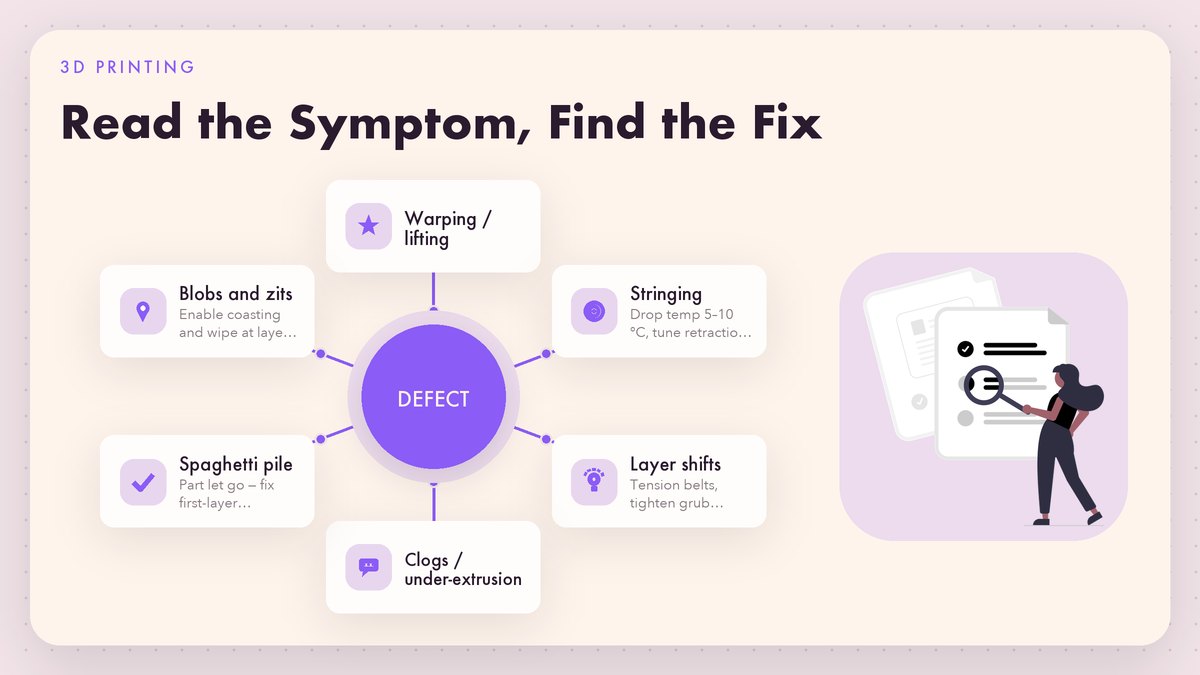
Every failed print is the machine writing you a diagnostic note — if you can read the symptom, you can usually name the cause in one guess. This is the symptom-first guide: warping, stringing, layer shifts, clogs, and the dreaded spaghetti, each matched to its real cause and the fix that actually works.
The first time my printer produced a plate of plastic spaghetti instead of a part, I assumed the machine was broken. It wasn’t. It was telling me, as clearly as it knew how, that the first layer had let go of the bed an hour earlier and nobody had noticed. Every defect in this hobby works that way: a visible symptom pointing at a specific cause, usually one you can fix in minutes once you know the translation. The Simplify3D print quality troubleshooting guide is the classic reference that taught a generation of owners to read their failures — this article is the symptom-first tour of the same skill.
One mindset note before the symptoms: change one thing at a time. Randomly flipping five settings between prints turns a solvable problem into an unsolvable one, because you can no longer tell which change helped. Diagnose, change, reprint, judge. Boring, and unbeatable. And keep the failed parts — a shelf of honorable failures, each labeled with what went wrong, is the fastest teaching collection this hobby offers. You’ll find yourself reaching for a past failure to identify a new one more often than you’d expect.
The Symptom Map
| Your print looks like… | Most likely cause | First fix to try |
|---|---|---|
| Corners lifting off the bed | Warping from uneven cooling or poor adhesion | Wash the plate, add brim, block drafts |
| Fine hairs between towers | Oozing filament during travel moves | Lower temperature 5–10 °C, tune retraction |
| Layers offset sideways mid-print | Loose belt, grub screw, or voltage dip | Tension the axis belt; tighten motor pulley screw |
| Thin, missing, or bubbly walls | Partial clog or wet filament | Cold pull; dry the spool |
| A tangled pile of loops (“spaghetti”) | Part let go of the bed hours ago | Fix first-layer adhesion; never walk away early |
| Rough surface with random bands | Inconsistent filament diameter | Try a better spool; check extruder tension |
| Small blobs/zits on walls | Pressure ooze at layer-change points | Enable “coasting”/”wipe” in the slicer |
Warping: The Corner-Lift Problem
The single most common way an overnight print dies
Plastic shrinks as it cools, and it shrinks more where it’s coldest. The bottom of your part is pinned to a heated bed while the top cools freely, so the top contracts harder — and the part’s corners peel upward like a potato chip. ABS warps worst (it shrinks the most, as covered in how FDM printing works); PLA and PETG warp far less but still lift when the conditions are wrong.
The fixes, in order of effort:
- Clean the plate. Skin oil defeats adhesion more often than geometry does. A quick wash with dish soap and water, fully dried, revives a “worn-out” surface for free.
- Add a brim. A 5–8 mm brim around the base adds grip area without changing the part. For small-footprint parts this alone solves it.
- Kill the drafts. Move the printer away from windows, vents, and fans. A $20 pop-up photo studio tent is a shockingly effective mini-enclosure for ABS-sized problems.
- Raise bed temperature and use the right surface. PETG at a lukewarm 50 °C lifts where 75 °C holds; glass with glue stick, PEI, or painter’s tape each grip differently by material.
Stringing: Fine Hairs Everywhere
Stringing happens when melted plastic drools out of the nozzle during travel moves. The two levers are temperature and retraction. Start by dropping the nozzle temperature 5–10 °C toward the low end of your spool’s range — less heat means thicker, less-runny ooze. If hairs persist, tune retraction: increase distance in 0.5 mm steps (or 1 mm on Bowden printers) up to the point where you hear no clicking from the extruder.
PETG stringers are the special case everyone meets eventually: they’re nearly universal because PETG is sticky when molten. For PETG, accept a little hair and keep a heat gun nearby — three seconds of warm air erases the wisps without touching the part. And whatever the material, check the obvious first: a nozzle caked in old plastic drags strands everywhere, and five minutes with a brass brush fixes what hours of retraction tuning won’t.
Layer Shifts: The Print That Walked Sideways
A layer shift means the printer lost track of where the head was — usually mid-print, producing a part whose upper half sits offset from its lower half like a botched magic trick. The cause is almost always mechanical:
- Loose belt on the shifted axis. Pinch the belt and pluck it: a healthy belt twangs; a loose one thuds. Tension adjusters fix this in two minutes.
- Loose pulley grub screw. The small gear on the motor shaft is held by one or two set screws, and if one is loose, the shaft spins without moving the belt — intermittently. Tighten both, and tighten the one against the shaft’s flat face.
- Binding or crashed part. If the printed part curls upward (see Warping), the nozzle eventually smashes into it and the motors skip steps. The shift is a symptom of the adhesion failure that came first.
- Voltage dip or cable snag. Rarer, but a power strip shared with a compressor, or a loose harness connector, can stall a motor for a moment. Rule out the first three before chasing this.
One diagnostic shortcut: shifts that happen at the same height on repeated prints point to binding at a specific position (a warped lead screw, a cable chain catching). Shifts at random heights point to looseness or voltage. The Marlin firmware documentation explains how the printer’s motion system counts and guards its position if you want the underlying mechanics. Also worth a quick check: disable “stealthChop”-style quiet modes while diagnosing — they’re a known source of lost steps on some drivers, and if your shifts vanish in normal mode, the mystery is solved before you touch a single belt.
Under-Extrusion, Clogs, and Wet Filament
The family of “not enough plastic” defects — thin walls, gaps between lines, a part that snaps apart along a band — shares three root causes. First, the partial clog: dust or a degraded chunk of plastic narrows the nozzle. The cold pull is the classic cure — heat the nozzle, push filament in, cool to around 90 °C, and yank; the plug comes out carrying the debris. Second, wet filament: plastics absorb moisture and then steam inside the nozzle, leaving bubbly, rough, weak sections — you’ll hear faint popping and hissing if you listen closely during the first layers. Drying the spool in a filament dryer (or a food dehydrator at low heat) for a few hours fixes it dramatically. Third, extruder trouble — a worn drive-gear tooth or wrong idler tension that slips on the filament, often audible as a rhythmic clicking from the extruder motor. The RepRap wiki has accumulated years of community knowledge on all three, worth keeping in your bookmarks.
Spaghetti: When the Part Let Go Hours Ago
The plastic-pile failure looks like a machine catastrophe but is usually an adhesion story that ended early: the part detached from the bed sometime after the first layers, and the printer cheerfully extruded into empty air for hours. Modern firmware can sometimes catch this with a “filament motion” sensor, but the reliable fix is behavioral — watch the first layer every time, and if you must leave, check the print remotely. Tools like OctoPrint with a webcam make this trivial, and it doubles as the answer to “did the overnight print survive?” without a trip to the garage.
Surface Blemishes: Blobs, Zits, and Ghosting
The last class of defects is cosmetic but annoying. Blobs and zits at layer-change points come from pressure still in the melt when a new layer starts — enable coasting (stop extruding slightly early) or a wipe move in the slicer, and most vanish. Ghosting — faint mirrored echoes after sharp corners — is vibration, and the fix is mechanical: slower outer-wall speed, firmer printer placement, and belts at proper tension. Rough, sandy-looking surfaces on a printer that used to print glossy almost always mean wet filament or a nozzle on its way to clogging, not a settings problem.
First-Layer Failures: Reading the Bottom of Every Print
Half of all troubleshooting is really first-layer troubleshooting, because the first layer is where adhesion, leveling, and cleanliness converge. Each classic first-layer look maps to one cause:
- Lines that round up like spaghetti and won’t merge: the nozzle is too high. The plastic never gets pressed into the plate, so it cools as separate strands. Re-level that corner — paper should drag with damp resistance.
- The nozzle plows a furrow and no plastic emerges: too close. The gap is smaller than the filament, so the flow blocks and the head drags a ridge. Back the corner off a quarter turn.
- Great adhesion on one side of the bed, hopeless on the other: the bed isn’t flat relative to the nozzle — the leveling pass needs a second trip around, because adjusting one corner moves the others.
- Adhesion was fine yesterday and terrible today: almost always surface contamination. One fingerprint-heavy batch of parts is enough. Wash the plate; don’t escalate to glue and tape while soap still works.
- The first inch of the outline won’t stick but the rest does: that’s a draft hitting the front corner, or the purge line dragging ooze into the path. Watch where the printer sits and whether the little start-up ooze gets picked up by the nozzle.
The deeper skill here is learning to check the first layer the way a pilot checks instruments: quickly, every time, before committing to the flight. A ten-second glance at minute two tells you whether the next six hours will produce a part or a science experiment.
When Nothing Works: The Reset Procedure
Occasionally a printer develops a defect that survives every targeted fix — stringing that no temperature change cures, banding that no belt tension removes, adhesion that survives only one print after cleaning. That’s the signal to stop treating symptoms and reset the whole system, because the problem is almost always something upstream that every individual fix assumed was fine:
- Swap the filament for a known-good spool. More “mystery defects” hide in a single bad roll of filament than in any printer component. If the problem vanishes with the swap, the spool — not the machine — was the defect.
- Restore the stock slicer profile. Years of accumulated tweaks become a pile of interacting settings nobody can reason about. A fresh profile for your exact printer model returns you to the state thousands of other owners print happily with.
- Re-run the mechanical pass. Frame square, belt tension, roller preload, grub screws. These drift invisibly over months of printing, and they undermine every downstream setting.
- Update firmware deliberately, not frantically. If the problem began right after a firmware update, that’s data — either a bug or a config migration issue. Klipper’s documentation and the Marlin docs both cover safe rollback and configuration checks; chasing hardware ghosts while the software changed underneath you wastes weekends.
The reset procedure feels like surrender the first time you do it. It isn’t. It’s how you trade a hundred unverifiable variables for five verifiable ones, and it resolves the majority of “haunted printer” cases within a single afternoon — often within the first step. The few cases that survive a full reset are genuinely rare, and they’re exactly the ones worth bringing to the manufacturer support forums with your clean, documented history in hand.
Overhangs and Bridging: When Gravity Wins
Two related defects confuse beginners because both look like “the plastic sagged.” Overhangs are sections where the layer below sticks out less than the current layer should — the plastic extrudes partly into air and, unsupported, droops. Bridges are long straight spans between two towers, printed across open air. Both are governed by cooling: the faster the plastic freezes after leaving the nozzle, the farther it can reach before gravity takes over.
The fixes, roughly in order of impact:
- Maximize part cooling. A stronger fan duct and 100% cooling fan for bridges is the single biggest improvement. Many stock printers ship with weak airflow aimed nowhere useful.
- Slow the print for overhangs. Modern slicers can detect overhangs and slow to 50% or less there, giving the fan time to freeze each strand before the next lands on it.
- Lower the temperature. Cooler plastic solidifies faster. The same temperature tower that tuned your material also reveals which end handles overhangs best.
- Redesign when you can. Orienting a model so its overhangs sit at 45 degrees or less often eliminates the problem entirely — and designing gentle slopes instead of sharp shelves is a free upgrade that no slicer setting can match.
One honest note: bridging longer than about 20 mm on a hobby printer rarely comes out pretty regardless of settings. For long spans, design in a support, split the model, or accept a sanding session — engineering around the limitation beats fighting it.
Building Your Troubleshooting Instinct
After a few months, this process becomes reflex: look at the failure, name the symptom, check the cheap causes first (cleanliness, temperature, tension), change one variable, reprint. The owners whose printers “just work” aren’t luckier — they’ve simply seen each of these failures enough times to skip the guessing. Keep a photo log of your failures with the fix that worked; six months from now, that log will be worth more than any settings spreadsheet, because it’s tuned to your machine, your filament, and your workshop. And when a friend buys their first printer and asks why everything is stringing, you’ll know the answer before they finish the sentence — which is, quietly, one of the better small pleasures this hobby hands out.
And when a symptom resists every fix in this guide — and occasionally one will — that’s the moment for the deeper references: the manufacturer support portals like Prusa’s official documentation, which maintain per-printer troubleshooting sections, and the calibration-first mindset from our companion guide, because a machine that’s out of calibration produces mystery defects that no symptom table can fully map.
External references checked October 2026: Simplify3D’s print quality troubleshooting guide, Wikipedia on fused filament fabrication, Marlin firmware documentation, the RepRap project wiki, OctoPrint documentation, and Prusa’s official support portal. Also in this series: first-printer setup and bed leveling, the calibration checklist, and the filament comparison.
Leave a Reply